
How Sodium Sulphate Is Manufactured
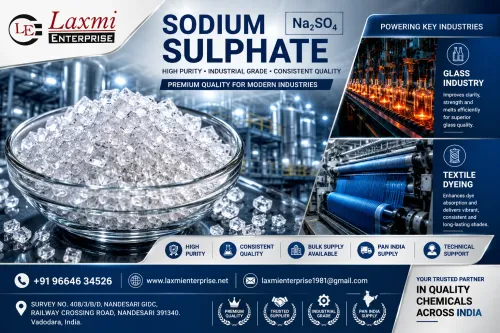
Every industrial chemical begins with a manufacturing process that determines its quality, consistency, and suitability for commercial applications. While sodium sulphate has the same chemical formula regardless of its source, the route used to produce it can influence its physical characteristics, impurity profile, particle size distribution, and overall product consistency.
For industrial buyers, understanding the manufacturing process is valuable because it provides insight into why different suppliers may offer products with varying specifications and performance. It also explains why laboratory testing and quality assurance are essential before material is approved for industrial use.
Rather than viewing sodium sulphate as a commodity, experienced procurement professionals evaluate the complete production process, quality systems, and consistency behind every batch.
Where Does Sodium Sulphate Come From?
Industrial sodium sulphate is generally obtained from two primary sources:
Natural sources
Industrial manufacturing or recovery processes
Although both routes produce sodium sulphate, the purification methods, quality control systems, and final product characteristics may differ.
Regardless of the source, the finished product should be manufactured under controlled conditions and verified through laboratory analysis before shipment.
Natural Sodium Sulphate
Natural sodium sulphate is obtained from naturally occurring mineral deposits and saline lakes where sodium sulphate has accumulated over long geological periods.
After extraction, the material normally undergoes several processing steps before becoming suitable for industrial applications.
Typical operations include:
Mineral extraction
Washing
Removal of unwanted impurities
Drying
Screening
Size classification
Packaging
Laboratory testing
Modern processing significantly improves the consistency and quality of naturally sourced sodium sulphate.
Industrially Manufactured Sodium Sulphate
In addition to natural deposits, sodium sulphate is also produced or recovered during various industrial chemical processes.
These manufacturing routes generally include:
Controlled chemical reactions
Recovery from industrial production streams
Purification
Filtration
Drying
Crystal formation
Screening
Quality verification
Industrial production emphasizes process control to achieve consistent product quality across multiple production batches.
Why Manufacturing Consistency Matters
From a procurement perspective, consistency is often more important than the manufacturing route itself.
A manufacturer capable of producing the same quality month after month offers significant advantages to industrial customers.
Consistent manufacturing provides:
Stable production performance
Reduced process adjustments
Predictable laboratory results
Reliable product quality
Lower rejection rates
Improved customer confidence
For continuous manufacturing industries, raw material consistency directly supports production efficiency.
The Typical Manufacturing Flow
Although manufacturing technologies vary between producers, the overall production sequence generally follows a structured workflow.
Typical Manufacturing Stages
Raw material selection
Chemical processing or mineral recovery
Purification
Solid-liquid separation
Drying
Particle size control
Quality inspection
Laboratory testing
Packaging
Dispatch approval
Every stage contributes to the final product quality.
Raw Material Selection
Quality begins long before laboratory testing.
Manufacturers carefully evaluate incoming raw materials because impurities present at the beginning of production can influence the finished product.
Typical quality considerations include:
Chemical composition
Purity
Moisture
Contamination
Consistency
Source reliability
Better raw material control usually leads to more consistent finished products.
Purification
Purification removes unwanted materials that may affect industrial performance.
Effective purification helps reduce:
Chloride impurities
Iron contamination
Insoluble matter
Foreign particles
Process residues
Well-controlled purification contributes to higher product consistency and customer satisfaction.
Drying
After purification, sodium sulphate is dried to achieve the desired moisture level.
Drying is an important production stage because excessive moisture may influence:
Storage
Flowability
Packaging
Handling
Product stability
Modern drying systems help manufacturers achieve consistent moisture levels before packaging.
Screening and Particle Size Control
Not every customer requires identical particle sizes.
Therefore, manufacturers often classify sodium sulphate according to customer specifications.
Particle size control improves:
Flowability
Dissolution
Automated feeding
Packaging consistency
Production efficiency
Screening also removes oversized or undersized particles.
Final Packaging
Packaging is more than simply filling bags.
It protects product quality during:
Storage
Transportation
Warehouse handling
Customer receiving
Long-distance shipping
Proper packaging minimizes contamination while helping maintain laboratory-approved quality.
Quality Control Throughout Manufacturing
Modern chemical manufacturing does not rely on final inspection alone.
Quality control begins before production starts and continues until the finished product is dispatched.
Typical quality checkpoints include:
Incoming raw material inspection
↓
Process monitoring
↓
Intermediate testing
↓
Drying verification
↓
Particle size inspection
↓
Laboratory analysis
↓
Packaging inspection
↓
Final release approval
This systematic approach helps ensure that customers receive consistent material.
Why Every Batch Is Tested
Even with advanced manufacturing equipment, no responsible manufacturer assumes every batch automatically meets specification.
Routine laboratory testing verifies product quality before dispatch.
Testing typically confirms:
Purity
Moisture
Chloride
Iron
Water insoluble matter
Particle size
Bulk density
Appearance
Only after satisfactory laboratory evaluation is the material approved for shipment.
Batch-to-Batch Consistency
Industrial buyers often discuss 'batch consistency.'
This refers to the manufacturer's ability to produce similar quality repeatedly over time.
Consistent batches help customers:
Maintain stable production
Reduce quality variation
Improve process control
Simplify inventory management
Reduce laboratory verification
Batch consistency is often one of the strongest indicators of manufacturing excellence.
Industrial Grades of Sodium Sulphate
Although the chemical formula remains the same, sodium sulphate is supplied in different grades to meet different industrial requirements.
Common commercial grades include:
Industrial Grade
Technical Grade
Commercial Grade
Application-specific grades
Each grade is developed according to customer expectations regarding purity, physical characteristics, and quality requirements.
The correct grade depends on the manufacturing process rather than simply selecting the highest available purity.
Why Different Industries Need Different Specifications
A common misconception is that every industry requires identical sodium sulphate.
In reality, manufacturing requirements vary significantly.
For example:
Detergent Industry
Often prioritizes:
Consistent particle size
Good flowability
Controlled moisture
Uniform packaging
Glass Industry
Typically emphasizes:
High purity
Low iron
Controlled chloride
Consistent chemical composition
Textile Industry
Usually focuses on:
Consistent quality
Reliable dissolution
Controlled impurities
Stable production performance
Chemical Manufacturing
Generally requires:
Predictable chemical composition
Reliable laboratory values
Batch consistency
Process stability
Understanding these differences allows suppliers to recommend the most appropriate product rather than a one-size-fits-all solution.
Why Manufacturing Quality Is More Important Than Low Price
Procurement decisions increasingly consider total manufacturing cost rather than purchase price alone.
A lower-priced product may appear attractive initially, but inconsistent quality can lead to:
Production downtime
Additional laboratory testing
Product rejection
Equipment cleaning
Higher waste
Customer complaints
Conversely, consistent raw materials often reduce hidden operational costs.
Experienced procurement teams therefore evaluate:
Supplier capability
Laboratory systems
Production consistency
Technical support
Documentation
Delivery reliability
before making purchasing decisions.
Frequently Asked Questions
1. How is sodium sulphate manufactured?
Industrial sodium sulphate is obtained from natural mineral deposits or produced through controlled industrial manufacturing and recovery processes. The finished product undergoes purification, drying, screening, laboratory testing, and packaging before shipment.
2. Is natural sodium sulphate better than synthetic sodium sulphate?
Not necessarily. Product performance depends more on purification, manufacturing controls, and laboratory quality than on whether the source is natural or industrially produced.
3. Why does manufacturing quality matter?
Consistent manufacturing produces reliable batches that improve production efficiency and reduce quality variation for industrial customers.
4. Why is purification important?
Purification removes unwanted impurities that may affect product performance, laboratory results, and customer satisfaction.
5. Why is drying necessary?
Drying helps achieve appropriate moisture levels, improving storage stability, packaging quality, and material handling.
6. Why is particle size controlled during manufacturing?
Different industries require different particle size distributions for optimal mixing, dissolution, handling, and automated feeding.
7. Why is every batch laboratory tested?
Routine laboratory testing verifies that each production batch complies with established quality specifications before dispatch.
8. What is batch consistency?
Batch consistency refers to the manufacturer's ability to produce similar quality repeatedly over time.
9. Why do industries require different grades?
Each manufacturing process has unique technical requirements, so sodium sulphate grades are selected based on application rather than a universal specification.
10. Does higher purity always mean better performance?
Not always. The most suitable grade is the one that matches the technical requirements of the customer's manufacturing process.
11. What should buyers evaluate besides price?
Buyers should assess product consistency, laboratory testing, technical documentation, packaging quality, delivery performance, and supplier reliability.
12. Why is supplier process control important?
Strong process control reduces quality variation, improves repeatability, and increases confidence in long-term supply.
13. Can two suppliers offer different quality even if both sell sodium sulphate?
Yes. Differences in raw materials, purification methods, process control, drying, and quality assurance can influence the final product.
14. What role does laboratory testing play after manufacturing?
Laboratory testing confirms that the finished product meets agreed specifications before it is released for shipment.
15. How does manufacturing consistency benefit customers?
It supports stable production, reduces process adjustments, minimizes quality complaints, and improves operational efficiency.